




UK – Alpesh Trivedi, Director of Magnetic International UK, explains how chemical-free water treatment can deliver a practical and effective solution for modern heat pump systems.
A new residential development in Newcastle-upon-Tyne has successfully implemented a chemical-free, two-stage heating water treatment solution to support the long-term performance of a heat pump and underfloor heating (UFH) system.
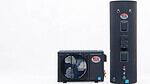
The project, delivered by Bill Hewison Bespoke Homes, featured a 15kW Stiebel Eltron heat pump installed in a newly constructed property. With local hard water conditions posing a known risk, Bill Hewison sought a reliable method to prevent scale formation, corrosion and system contamination, without relying on traditional chemical dosing.
The challenge
Closed-loop heating systems, particularly those incorporating heat pumps and UFH, are highly sensitive to water quality. Dissolved minerals in hard water can lead to scale build-up on plate heat exchangers, while oxygen ingress during top-up can accelerate corrosion and generate magnetite. In addition, many heat pump manufacturers specify strict water quality requirements. Failure to comply can result in reduced system efficiency, component damage, and potential warranty issues.
The project required a solution that would:
• Meet manufacturer water quality requirements
• Avoid reliance on chemical inhibitors
• Be simple to install and maintain on-site
• Support long-term system performance
The solution
Working with Magnetic International UK, a two-stage demineralised water strategy was implemented:
Initial System Fill
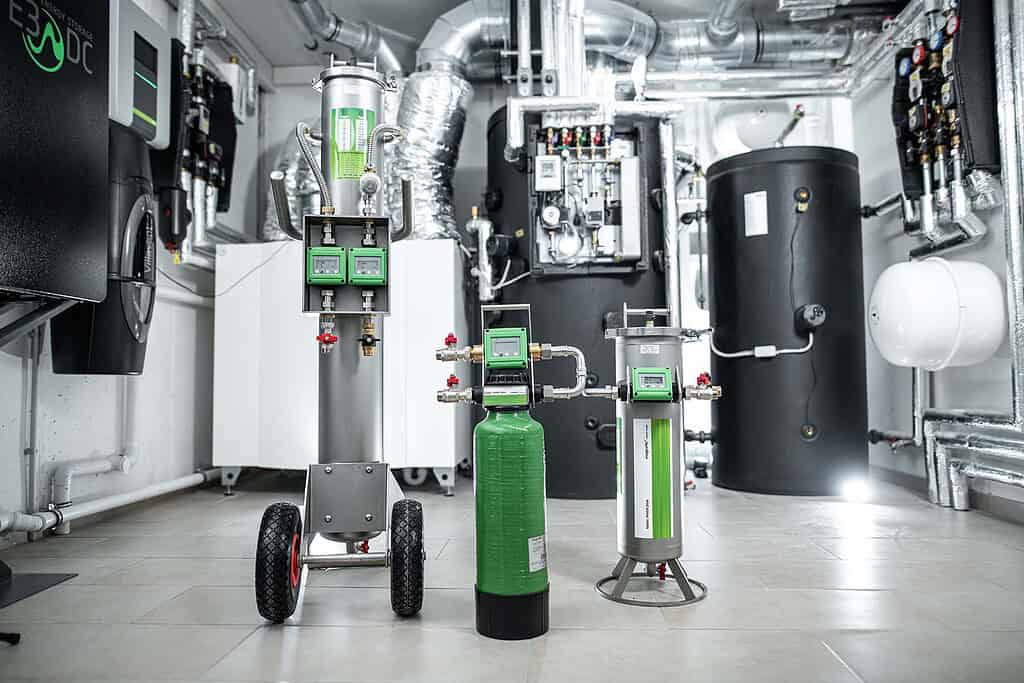
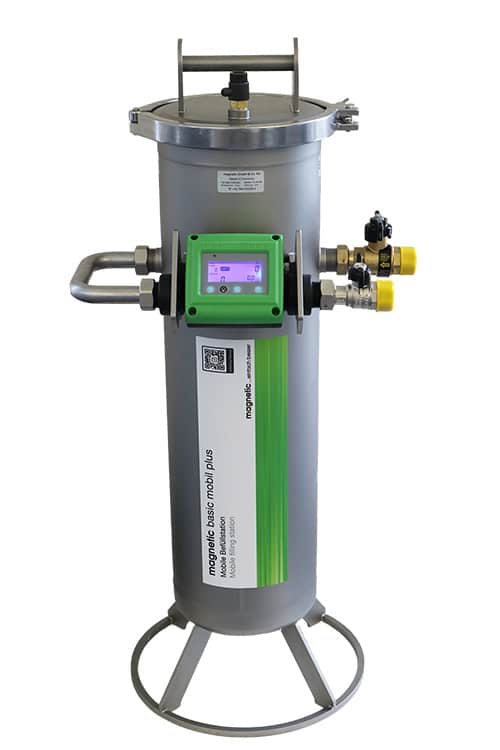
Magnetic’s basic mobile plus unit, above, was used to charge the system with demineralised water, ensuring low conductivity and minimal mineral content from the outset. The unit includes integrated monitoring to verify water quality during filling.
Ongoing Top-Up Protection
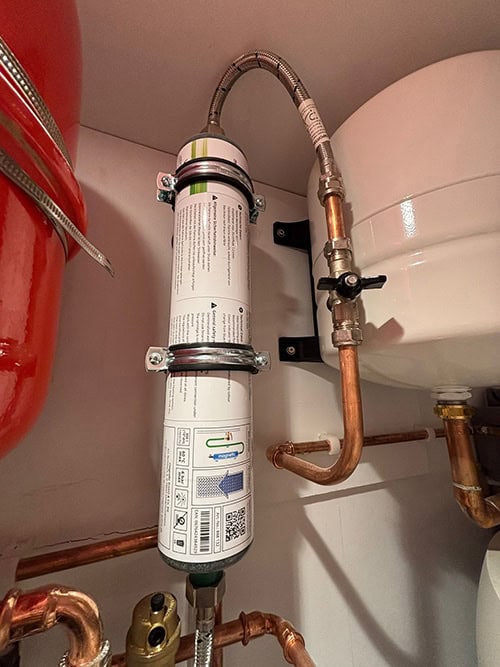
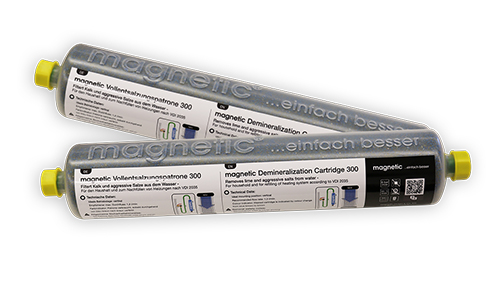
A compact demineralisation cartridge was installed on-site, above, to treat any future top-up water. This ensures that additional water entering the system does not introduce minerals or oxygen-related risks. The cartridge features a visual indicator, enabling service engineers to easily identify when replacement is required.
The results
The system was successfully commissioned using demineralised water, aligning with manufacturer guidance and industry best practice including VDI 2035.
Key outcomes include:
• Reduced risk of scale and corrosion
• Protection of heat exchangers and system components
• Simplified maintenance without chemical dosing
• Improved long-term reliability and efficiency
• Maintained manufacturer warranty compliance
Conclusion
Magnetic International UK believes this project demonstrates how a chemical-free, two-stage water treatment approach can provide a practical and effective solution for modern heat pump systems. By combining controlled initial filling with protected top-up, installers can maintain water quality throughout the system lifecycle, supporting both performance and compliance without adding operational complexity.


